Maintaining consistent temperature control across multiple shifts is a challenge in 24/7 injection molding operations due to factors such as ambient temperature changes, operator variability, and controller drift. The first step is to standardize the setup procedure. Create a detailed checklist that includes the setpoint for each zone, the PID parameters, and the expected steady-state temperature. This checklist should be followed at every shift change. Use a "template" system in the controller where the settings for each mold are saved and can be loaded with a single command. This eliminates manual entry errors. The second step is to implement a "warm-up" routine. If the hot runner is turned off between shifts, the warm-up protocol must be consistent: a defined ramp rate (e.g., 5°C/min) and a hold time at standby before starting production. Inconsistent warm-up can lead to different thermal expansion and seating of the thermocouple, affecting readings. The third step is to use automatic temperature compensation. Many controllers have a feature that automatically adjusts the setpoint based on the ambient temperature measured at the cold junction. If the factory gets hotter during the day, the controller can raise the setpoint slightly to maintain the same melt temperature. This compensation must be calibrated correctly. The fourth step is to establish a "temperature verification" routine at the start of each shift. Use a portable pyrometer or a reference thermocouple to check the nozzle tip temperature against the controller's reading. If a deviation is detected, the operator can adjust the controller's offset. This check takes only a few minutes but prevents drift-related quality issues. The fifth step is to train operators on the signs of temperature instability-such as increased flash or short shots-and empower them to adjust the temperature within a defined range (e.g., ±2°C). Have a clear escalation path for deviations outside this range. The sixth step is to use data logging. Record the temperature of each zone every minute and store the data. At shift change, the incoming shift can review the previous shift's temperature chart. If the temperature was trending up or down, they can investigate and correct before production continues. The seventh step is to ensure consistent cooling water temperature and flow, as variations in cooling can affect the thermocouple's reading (via heat sinking). Install a temperature control unit on the water circuit and monitor it. The eighth step is to schedule thermocouple calibration and replacement at regular intervals, rather than waiting for failure. This removes the variability of aging sensors. By combining standardization, automation, training, and monitoring, multi-shift plants can achieve temperature control that is as consistent as if one operator managed every shift, leading to stable part quality and reduced scrap.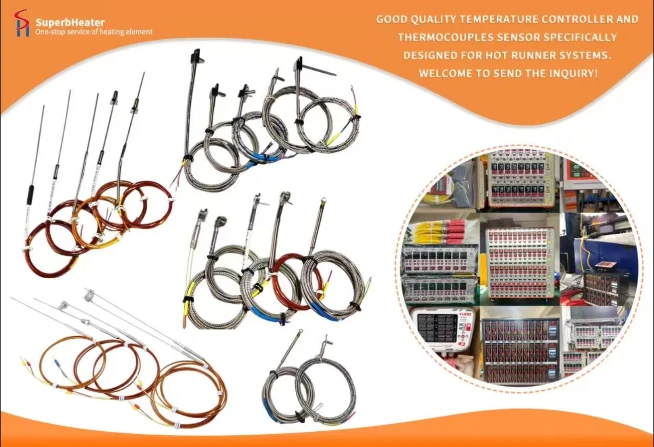

 English
- English
- Français
- Deutsch
- 日本語
- Italiano
- Español
- Português
- русский
- Indonesia
- عربي
- Ελληνικά
- Polski
- فارسی
- עברית
- Kreyòl Ayisyen
- 한국어
- Türkçe
- slovenčina
- Bai Miaowen
- Cymraeg
- dansk
- Lietuvių
- Malti
- Svenska
- Srbija jezik (latinica)
- O'zbek
- ไทย
- suomi
- magyar
- Eesti
- Català
- slovenščina
- Melayu
- Български
- اردو
- România limbi
- bosanski
- हिंदी
- Gaeilgenah Éireann
- Việt Nam
- বাংলা
- íslenska
- Norsk
- Latviešu
- hrvatski
- Nederlands
- Čeština
- українська


