The plasticization phase is the process of melting the resin in the screw barrel. While the thermocouple in the hot runner does not directly measure the plasticization temperature, it can provide feedback to optimize the plasticization process. The first step is to establish a relationship between the plasticization parameters (back pressure, screw speed) and the hot runner temperature. A higher back pressure or screw speed generates more shear heat, which increases the melt temperature. The thermocouple in the hot runner nozzle will show a higher temperature. The second step is to establish a baseline. Run the process at the nominal plasticization parameters and record the hot runner temperature. The third step is to use the hot runner temperature to adjust the plasticization parameters. If the hot runner temperature is too high, reduce the back pressure or the screw speed. If it is too low, increase them. The fourth step is to use a "closed-loop" control. The controller adjusts the back pressure or screw speed in real time based on the hot runner temperature, maintaining a constant melt temperature. The fifth step is to use the hot runner temperature to detect variations in the material. If the material has a different melt viscosity, the hot runner temperature will change. The thermocouple data can be used to detect these variations and trigger a material check. The sixth step is to use the hot runner temperature to optimize the plasticization time. A shorter plasticization time increases the shear heat, raising the hot runner temperature. The goal is to find the shortest plasticization time that still produces a melt of the correct quality. The thermocouple data is used to guide this optimization. The seventh step is to use the hot runner temperature to detect a screw wear issue. A worn screw may not melt the material effectively, resulting in a lower melt temperature at the nozzle. The thermocouple data will show a lower temperature. The eighth step is to integrate the thermocouple data with the barrel temperature control. By combining the barrel temperature and the hot runner temperature, the plasticization process can be more precisely controlled. By using hot runner thermocouple data to optimize the plasticization phase, molders can improve the melt quality and reduce the energy consumption of the plasticization process.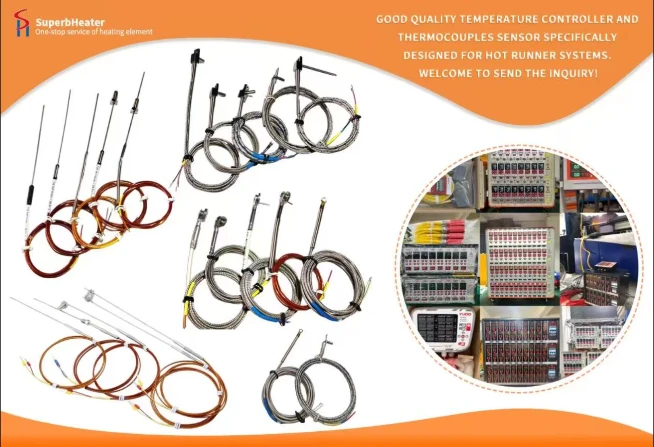

 English
- English
- Français
- Deutsch
- 日本語
- Italiano
- Español
- Português
- русский
- Indonesia
- عربي
- Ελληνικά
- Polski
- فارسی
- עברית
- Kreyòl Ayisyen
- 한국어
- Türkçe
- slovenčina
- Bai Miaowen
- Cymraeg
- dansk
- Lietuvių
- Malti
- Svenska
- Srbija jezik (latinica)
- O'zbek
- ไทย
- suomi
- magyar
- Eesti
- Català
- slovenščina
- Melayu
- Български
- اردو
- România limbi
- bosanski
- हिंदी
- Gaeilgenah Éireann
- Việt Nam
- বাংলা
- íslenska
- Norsk
- Latviešu
- hrvatski
- Nederlands
- Čeština
- українська


