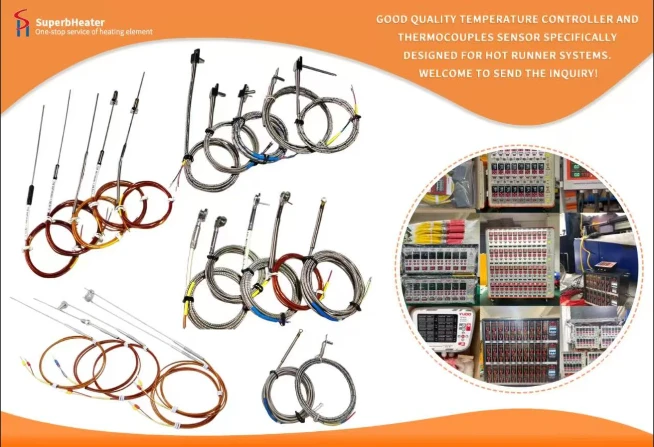
Improper installation accounts for over 65% of premature thermocouple failures in hot runner systems. Standardized mounting processes eliminate mechanical stress, poor contact, and signal interference, potentially doubling average sensor service life. This article details the installation specifications that extend thermocouple life.
Manifold Pin Thermocouple Installation. The reserved mounting hole diameter must match the sheath outer diameter with clearance ≤0.1 mm. Oversized holes create loose fit and variable contact pressure during thermal expansion. Hole depth must reserve 1–2 mm spring compression travel for bayonet probes, ensuring the spring fully presses the sensing tip against the hole bottom after thermal expansion. Insufficient travel causes gap heat loss and low reading deviation. Insert the probe straight without lateral extrusion-bending during insertion generates internal wire fatigue cracks. After insertion, tighten compression fittings evenly to avoid sheath deformation. The correct insertion depth for manifold thermocouples is two-thirds of the reserved hole depth.
Hot Nozzle Integrated Thermocouple Assembly. When installing coil heater sleeves with embedded thermocouples, avoid twisting the built-in sensing wire during sleeve rotation-torsion force fractures internal alloy wires rapidly. Align the thermocouple wire outlet with the mold wire channel to prevent sharp edges cutting cable outer braids. Do not pull the thermocouple cable hard when removing the nozzle; hold the heating sleeve body instead of the wire section. Nozzle thermocouples must be close to the effective heating section to ensure the probe is in the optimal temperature sensing area.
Cable Wiring and Anti-Interference. Thermocouple signal cables must be laid separately from high-current heater power cables, with spacing above 30 mm. Bundling signal and power wires together induces severe electromagnetic noise and temperature jumping readings. Shielded thermocouple braided cables should only be grounded at the temperature controller end-double-end grounding creates ground loop drift faults. Avoid excessive cable bending; minimum bending radius shall not be less than 5 times the sheath diameter. Route cables away from mold cooling water channels to eliminate cold end temperature fluctuation affecting measurement accuracy.
Connector and Cold Junction Installation. Thermocouple plugs must be installed on the mold outer surface instead of inside high-temperature mold plates to keep cold junction temperature stable. Internal high-temperature placement accelerates plug terminal oxidation and polarity short circuits. Tighten plug terminal screws evenly, and remove white oxide powder on terminals during regular maintenance. Mark each zone plug with corresponding heating zone numbers to avoid cross-wiring during replacement.
Post-Installation Inspection. After full assembly, conduct multimeter continuity testing to rule out open circuits. Power on the temperature controller for low-temperature preheating (80°C holding for 30 minutes) before raising to production temperature-avoiding rapid thermal shock protects newly installed thermocouples. Record installation date for each probe to arrange periodic replacement plans. Store spare thermocouples in dry constant-temperature cabinets to prevent sheath rust and wire oxidation. Strict implementation of these specifications reduces thermocouple failure rates by over 60%.