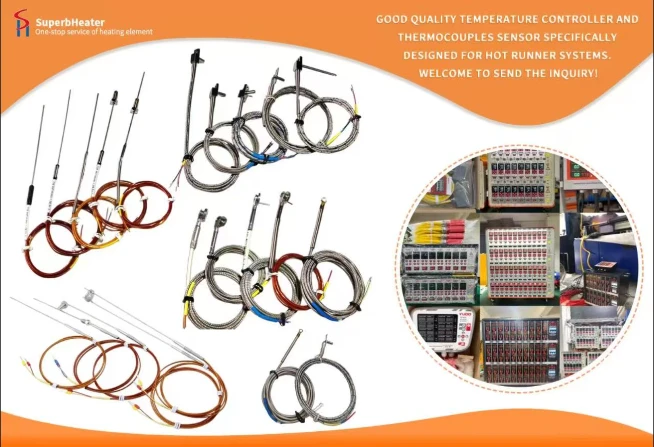
Valve gate hot runner systems add a layer of complexity with actuated pins that open and close the gate. Temperature control in valve gates is even more critical than in open systems because pin movement and gate sealing depend on thermal expansion and melt viscosity. Thermocouples play distinct roles in this environment.
Multiple Temperature Zones in Valve Gates. A typical valve gate nozzle has two or three heating zones: the main body, the tip, and sometimes the gate area. Each zone has its own thermocouple. The main body thermocouple controls bulk melt temperature; the tip thermocouple ensures the melt is at the right viscosity for injection; and the gate thermocouple (if present) controls the region where the pin seals, preventing drool or freeze-off.
Pin Thermal Expansion Management. Valve pins are made of tool steel or ceramics. They expand when heated. If the pin expands too much, it may jam or not seal properly. The nozzle body also expands. Thermocouples monitor the temperature differential between the pin and the housing. Advanced controllers use this data to modulate the tip heater to maintain the pin at a temperature that ensures proper clearance. Without accurate thermocouples, pin jamming is common.
Gate Sealing Temperature. The valve pin tip must seal against the gate orifice at the end of injection. If the tip is too hot, the plastic may not freeze off quickly, causing drool (stringing). If too cold, the pin may stick to the gate or cause cold slug. The tip thermocouple is crucial for maintaining the gate seal temperature-often 30–50°C below the melt temperature. This narrow window requires a fast, accurate thermocouple near the pin tip.
Sequential Valve Gating. In large parts or family molds, valve pins open sequentially to control weld line position and packing. Each nozzle's thermocouple must report temperature individually so that the controller can time the valve opening based on thermal conditions. If one zone is slightly cooler, its valve may open later to ensure flow. Thermocouple data thus directly affects the timing algorithm.
Thermal Cycling During Valve Operation. Each cycle, the valve pin moves in and out. This mechanical movement can cause friction and local heating. The thermocouple near the guide bushing may detect this heat, providing feedback to adjust cooling or reduce friction. In high-cycle applications, the tip thermocouple may see temperature spikes of 10–20°C at valve actuation; the controller must compensate quickly.
Pressure and Temperature Coupling. Valve gate nozzles experience high injection pressures (up to 2000 bar) that can deform the nozzle body, potentially affecting thermocouple contact. Spring-loaded thermocouples are essential to maintain contact despite deflections. Also, pressure-induced temperature changes (adiabatic heating) can be sensed by fast thermocouples, allowing the controller to anticipate melt temperature rises and reduce power preemptively.
Fault Detection in Valve Systems. Thermocouples help diagnose valve problems. If a valve pin sticks, the melt may stagnate around it, causing the thermocouple to read a different temperature pattern (e.g., slower response to setpoint changes). A deviation between the tip thermocouple and the body thermocouple of more than 15°C may indicate poor heat transfer due to pin binding. This data can trigger maintenance alerts.
Installation Challenges in Valve Nozzles. The presence of the valve pin limits space for thermocouple placement. Sheath diameters often must be 1.0 mm or smaller to fit between the pin bore and the heater. Such thin probes are fragile and require careful handling. Some designs place the thermocouple inside the valve pin itself (via a hollow pin), but this is expensive. More common: a side-entry probe just below the tip, angled to avoid the pin.
Integration with Valve Controllers. Modern valve gate controllers receive thermocouple inputs for each nozzle and also monitor valve position sensors. They use a cascade control strategy: the temperature loop sets the heater power, and the valve timing loop uses temperature to adjust opening/closing delays. This integrated control ensures consistent part weight and dimensions, especially in multi-cavity molds.
Typical Setpoints. For polypropylene, the tip temperature is often set 20°C below the body to promote gate freeze. For nylon, the differential may be 30°C to prevent drool. Thermocouple accuracy of ±1°C is necessary to maintain these differentials. Use Class 1 sensors in valve gate applications.
Preventive Maintenance. Because valve pins move, they can abrade the thermocouple sheath over time. Inspect tip thermocouples every mold cleaning cycle. Look for flattening or scoring on the sheath. Replace if any wear is visible, as a worn sheath can expose the thermoelements to melt, causing catastrophic failure.
Case Study: Stringing Problem. A molder of thin-wall containers experienced stringing at the gate. The tip thermocouple was reading 10°C higher than actual (drift). The controller kept the tip too hot, preventing freeze-off. After recalibration and replacement, the tip temperature was correctly set 20°C below melt, stringing disappeared, and cycle time reduced by 0.3 seconds.