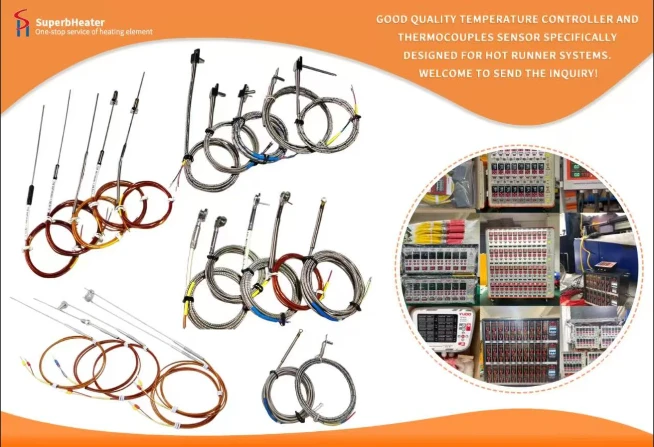
Torque specifications for thermocouple installation are not optional suggestions-they are critical parameters that directly affect sensor performance, service life, and warranty validity. Improper torque is one of the most common-and most costly-installation mistakes in injection molding. All major hot runner manufacturers publish strict, specific installation guidelines including torque limits designed to ensure safe, reliable operation.
The Consequences of Improper Torque. Over-tightening can crush the sheath or damage internal insulation, leading to open or short circuits. Under-tightening results in poor thermal conduction, causing slow response and inaccurate readings. Ignoring torque specifications for fittings leads to loose contact or physical damage. In many cases, improper installation causes immediate failures such as short circuits, heater burnout, manifold cracking, or plastic leakage.
Standard Torque Ranges by Thread Specification. For thermocouple threaded connections, torque must be strictly controlled according to thread specifications. M12×1.5 threads require 8–12 N·m, suitable for small sensors such as mold temperature measurement points. M14×1.5 threads require 12–15 N·m, commonly used in the middle section of the barrel or hot runner plate sensors. M16×1.5 threads require 15–20 N·m for larger sensors in high-temperature areas. Custom non-standard threads must follow manufacturer instructions.
Manifold Button Thermocouple Torque. For manifold button thermocouples, the compression screw should be tightened with a torque wrench at 1.2–1.5 N·m. Excessive force will cause sheath deformation, while insufficient force will lead to loose contact. Before installation, use abrasive cloth to polish the manifold mounting plane to remove rust and carbon plastic deposits, then apply a thin layer of high-temperature thermal conductive silicone paste on the brass measuring base.
Mold-Masters Specific Torque Values. According to Mold-Masters documentation, shoulder head screws attaching valve pin holders to pistons should be tightened to 3 N·m (2.2 lbf-ft). Adapter mounting screws require 7 N·m (5 lbf-ft). Gate seals must be torqued in heated condition at processing temperature as specified in the General Assembly drawing.
Critical Operating Principles. A torque wrench must always be used-manual tightening based on experience is strictly forbidden. Insufficient torque causes sensor loosening (poor temperature measurement contact, vibration shedding), while over-tightening causes probe deformation such as cracking of the thermocouple ceramic insulation layer or thread stripping. If M16 thread exceeds 25 N·m, it may cause the stainless steel probe and mounting hole threads to seize, making later disassembly difficult.
Material Compatibility Considerations. When the sensor (stainless steel) is threaded with equipment components such as aluminum alloy molds, an anti-seizing agent (such as molybdenum disulfide grease) must be applied to the thread surface, and torque should be applied at 90% of the recommended value to avoid electrochemical corrosion and difficulty in disassembly.
Warranty Implications. Hot runner suppliers often require proof of professional installation and use of approved components to honor warranty claims. Over-tightening thermocouple probes cracks nozzle seats, deforms sensor structures, or destroys internal junctions. These errors void warranties and leave manufacturers liable for expensive repairs.