Process variation-unexpected changes in part quality-is a major challenge in injection molding. Analyzing thermocouple data is a powerful way to identify the root cause. The first step is to collect high-quality data. Ensure that the thermocouple signals are clean (low noise) and that the data is logged at a sufficient rate (e.g., every second). The data should include the temperature reading, the setpoint, and the heater power percentage for each zone. The second step is to perform a time-series analysis. Plot the temperature data over time (e.g., over a day or a week). Look for patterns: a gradual drift, a sudden step change, or periodic oscillations. A gradual drift (e.g., 0.1°C per day) indicates a slowly degrading thermocouple or heater. A sudden step change (e.g., after a mold change) indicates an installation error. Periodic oscillations (e.g., cycling every 5 minutes) suggest a control loop instability or a cyclic disturbance (like an air conditioner turning on). The third step is to correlate with part quality. If parts are rejected, check the thermocouple data at the time the parts were produced. If a zone's temperature was different from its baseline, it is the likely cause. For example, if the part weight is consistently high when zone 2 is 1°C above the setpoint, the correlation is established. The fourth step is to analyze the power percentage. A zone that requires more power to maintain the setpoint is losing heat (or has a failing heater). A zone that requires less power may have a thermocouple that is reading high (drift). The fifth step is to use a statistical process control (SPC) chart. Plot the temperature of each zone on an X-bar/R chart. If a data point falls outside the control limits, it indicates a special cause variation. Investigate the cause. The sixth step is to perform a "cause-and-effect" analysis. For each zone, list all possible causes of temperature variation: thermocouple drift, heater failure, cooling water changes, ambient temperature changes, material changes, and mold changes. Use the thermocouple data to eliminate causes. The seventh step is to use a "fault tree" analysis. Start with the symptom (e.g., part weight variation) and work backwards to the possible causes, using the thermocouple data to assign probabilities. The eighth step is to document the findings. Record the root cause (e.g., thermocouple drift in zone 3) and the corrective action (e.g., replace zone 3 thermocouple). This becomes a part of the plant's knowledge base for future troubleshooting. By systematically analyzing thermocouple data, engineers can pinpoint the root cause of process variations, leading to effective corrective actions and preventing recurrence. This data-driven approach is far more efficient than trial-and-error.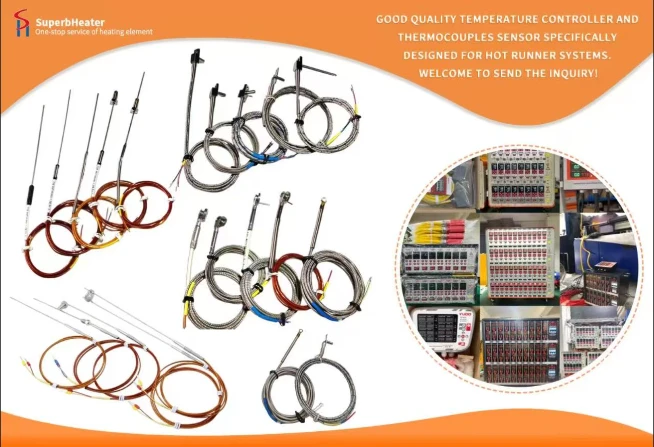

 English
- English
- Français
- Deutsch
- 日本語
- Italiano
- Español
- Português
- русский
- Indonesia
- عربي
- Ελληνικά
- Polski
- فارسی
- עברית
- Kreyòl Ayisyen
- 한국어
- Türkçe
- slovenčina
- Bai Miaowen
- Cymraeg
- dansk
- Lietuvių
- Malti
- Svenska
- Srbija jezik (latinica)
- O'zbek
- ไทย
- suomi
- magyar
- Eesti
- Català
- slovenščina
- Melayu
- Български
- اردو
- România limbi
- bosanski
- हिंदी
- Gaeilgenah Éireann
- Việt Nam
- বাংলা
- íslenska
- Norsk
- Latviešu
- hrvatski
- Nederlands
- Čeština
- українська


