Multi-color sequential co-injection molds employ independent layered hot runner manifolds to inject different colored resins, soft-hard composite elastomers, and transparent base materials in separate molding strokes. Each flow channel system operates under distinct temperature windows, corrosive gas release levels, and spatial layout limits. Conventional unified sensors cannot adapt to segmented temperature control demands.
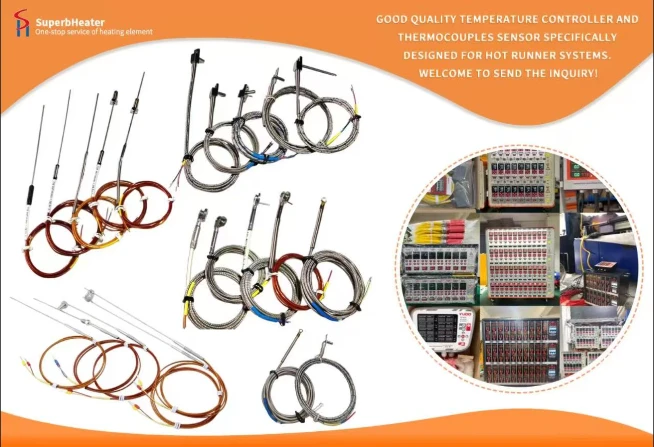
Material-Based Alloy and Sheath Selection. Hard engineering plastic flow channels (ABS, PC, PA66) with processing temperatures of 260–320°C adopt standard Class 1 K-type thermocouples with mirror-polished 316L stainless steel sheaths. Soft TPE and TPU elastomer manifolds running at 170–230°C select high-sensitivity Type E thermocouples, whose twice-higher low-temperature signal sensitivity captures tiny temperature fluctuations to prevent elastomer thermal decomposition.
Corrosive Material Requirements. Manifolds for flame-retardant, POM, and halogen-modified color masterbatch materials generate acidic and sulfide volatile gases during melting. These require Hastelloy alloy sheath probes to resist pitting corrosion-ordinary 304 steel sheaths will perforate within one month of continuous co-injection production.
Optical Material Specifications. Transparent PMMA and optical PC co-injection circuits deploy oil-free ultra-clean thermocouples with full vacuum-sealed hot junctions, eliminating metal ion precipitation that damages product light transmittance. J-type iron-containing probes are completely banned for all multi-color co-injection molds, as iron alloy wires rapidly oxidize under alternating heat and corrosive gas exposure, triggering severe irreversible temperature drift.
Spatial Layout Customization. Two groups of manifolds in sequential co-injection molds are closely stacked with narrow gaps reserved for wiring. L-shaped and Z-shaped bent miniature mineral-insulated thermocouples with 0.5–1.0 mm thin walls are customized according to mold 3D drawings, with bending radii strictly controlled above 8 times sheath diameter to avoid internal wire fatigue fracture.
Independent Channel Configuration. Each material's manifold and nozzle heating zone must be equipped with exclusive thermocouples. Sharing a single probe between high-temperature hard plastic and low-temperature elastomer circuits will cause fatal temperature imbalance-the hard plastic zone continuously overheats the soft material melt to trigger decomposition, while the hard substrate fails to reach sufficient melting temperature.