Bi-color co-injection molds employ two independent hot runner systems to inject different raw materials sequentially. The dual thermocouple systems interfere with each other in signal transmission, and unreasonable layout easily causes temperature crosstalk between first and second injection hot runners. Optimized layout schemes are essential for preventing delamination, flow marks, and fusion defects.
Physical Isolation of Two Systems. The core principle is physical isolation and signal separation of the two temperature sensing systems. The first and second injection manifolds are installed on the rotating middle plate with narrow spacing between the two groups. All thermocouple wire grooves of Group A and Group B must be completely separated by steel isolation partitions, with no overlapping or crossing of wire harnesses.
Minimum Safety Distance. The minimum safety distance between measuring probes of the two hot runner systems must be kept above 25 mm to avoid heat conduction mutual interference between adjacent measuring points. If probes are arranged too closely, heat conduction interference will make the temperature of one system follow the other, requiring re-drilling of measuring holes to increase spacing to over 25 mm.
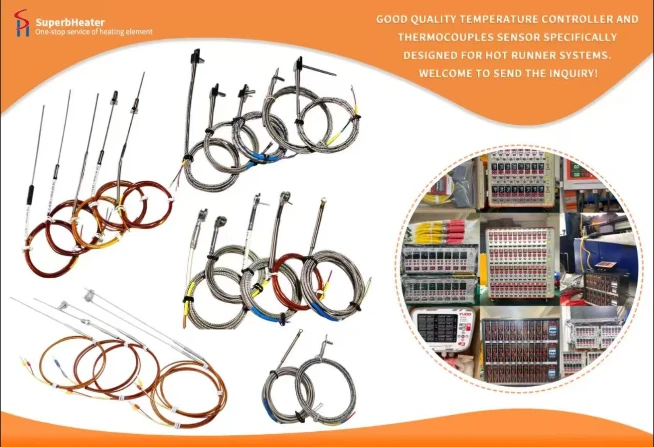
Shielding Requirements. All ungrounded double-shielded thermocouples should be uniformly selected for both sets of hot runners to suppress cross-system electromagnetic induction signals. Each group independently arranges front, middle, and tail distributed button thermocouples without sharing temperature compensation signals between the two systems.
Independent Temperature Control. The melting temperature windows of two raw materials for bi-color products are often different-for example, hard PC outer layer and soft TPU inner layer require independent temperature curve control. Separate multi-point layout ensures that each runner branch of both materials maintains stable melt viscosity, solving poor interface fusion caused by inconsistent temperatures during sequential injection.
Special Wiring for Rotating Plates. Bi-color molds rely on rotating plates to switch injection stations, and thermocouple wires between the fixed template and rotating plate bear periodic torsion and tensile force every molding cycle. Conventional fixed-length wire harnesses are prone to twisting, abrasion, and fracture after thousands of rotations. Customize ultra-soft long mineral-insulated thermocouple wires, reserve more than 350 mm loose wire margin at the rotating joint, and install wear-resistant rotary wire protection sleeves.
Common Faults and Solutions. If two groups of thermocouple wire harnesses share the same wire groove without isolation partitions, synchronous jumping of temperature readings between first and second injection zones will occur. Add 5 mm thick steel isolation baffles to separate the two wire channels. If wire allowance at the rotating plate is insufficient, replace with customized long soft wires and install rotary protection sleeves to eliminate tensile stress.