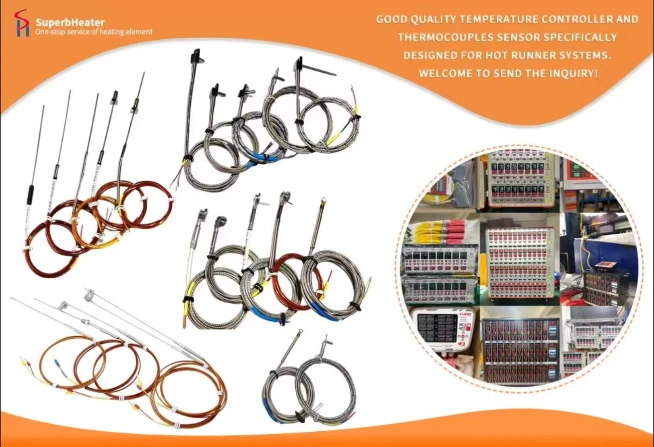
Connectors are the weakest link in the thermocouple signal chain. Poor contacts, corrosion, or wrong alloy cause more errors than the sensor itself. This article provides best practices for selecting and maintaining thermocouple connectors.
Alloy Compatibility. Connector pins must be made of the same thermocouple alloy as the sensor (e.g., chromel-alumel for Type K). Using copper or brass pins introduces a junction error. Premium connectors use thermocouple-grade alloys. Verify this with the supplier. The connector housing should also be rated for the ambient temperature (typically >200°C for hot runner applications).
Color Coding. Connectors and cables should be color-coded per thermocouple type: Type K – yellow; Type J – black; Type T – blue; Type N – orange. Ensure the connector housing matches the cable color. Polarity should be marked on the connector: positive (red or yellow) and negative (black or white). This prevents wiring errors.
Connector Types. Several connector styles are used in hot runners: miniature standard plugs (e.g., flat pins), heavy-duty rectangular connectors (Harting, Wieland), and circular connectors (e.g., military-style). Choose a type that is durable, easy to disconnect, and provides good strain relief. For frequent mold changes, quick-disconnect circular connectors are recommended.
Temperature Rating. The connector must withstand the heat radiating from the mold. Standard connectors are rated to 120°C, high-temperature versions to 200°C or more. If the junction box near the mold exceeds 100°C, use high-temperature connectors. Also, ensure the cable insulation (silicone or fiberglass) matches the temperature.
Strain Relief. Vibration and cable movement stress the connection. Use connectors with built-in strain relief (clamps or boots) to prevent wire pullout. Secure the cable near the connector with a tie wrap. This prevents the connection from being the point of failure due to mechanical strain.
Sealing. Moisture and contamination degrade connector contacts. Use connectors with grommets or seals (IP65 or higher). Apply dielectric grease to the pins before mating-this prevents corrosion and eases disconnection. For outdoor or high-humidity environments, sealed connectors are mandatory.
Contact Pressure. Pins must maintain adequate contact pressure. Over time, spring tension decreases, causing intermittent connections. Use connectors with gold-plated contacts (gold resists oxidation and maintains low resistance). Replace connectors if they feel loose during mating.
Soldering vs. Crimping. Crimped connections are more reliable than soldered ones in high-vibration environments. Soldering can wick the thermocouple wire, changing its alloy composition at the junction. Use crimp terminals with the correct tool. If soldering is unavoidable, use a low-temperature solder and heat sink to prevent alloy change.
Polarity Verification. Before using a new connector, verify polarity with a multimeter. Connect the thermocouple to a reference probe, heat the tip, and check that the voltage polarity matches the connector marking. This simple test catches factory errors.
Regular Inspection. During preventive maintenance, inspect connectors visually: look for bent pins, corrosion, discoloration, or melting. Clean contacts with a contact cleaner and a soft brush. Check that the connector shell is tightly closed. Replace any damaged connector immediately.
Replacement Cycles. Connectors age with thermal cycling. Plan to replace connectors every 2–3 years, even if they appear functional. The plastic housing becomes brittle, and spring tension decreases. Combining connector replacement with thermocouple replacement simplifies logistics.
Standardization. Standardize connectors across all molds where possible. Use the same type, pin layout, and color coding. This reduces inventory and training. If you have multiple plants, standardize globally. Work with your connector supplier to achieve this.
Locking Mechanisms. Use connectors with locking latches or screw rings. These prevent accidental disconnection from vibration. Push-fit connectors are too loose for hot runner applications; always choose positive-locking designs.
Case Study: Intermittent Errors. A plant experienced sporadic temperature spikes on one zone. The problem persisted despite replacing the thermocouple. Investigation revealed a loose pin in the connector housing-it made contact only when the cable was in a certain position. Replacing the connector solved the issue.
Spare Connectors. Keep pre-wired connector assemblies for each mold. This allows quick replacement during emergencies. Pre-wire connectors in the maintenance shop, not at the machine, to ensure quality. Label each assembly with zone number and thermocouple type.
Supplier Qualification. Qualify connector suppliers by testing their products in your environment. Look for connectors that maintain low contact resistance (<0.1 Ω) after 1000 mating cycles. A reputable supplier will provide durability data.
Tooling. Use the correct crimping and stripping tools. Using the wrong tool damages the wire or creates a cold joint. Invest in quality tools and train technicians on their proper use.
---